
What Is Fretting?
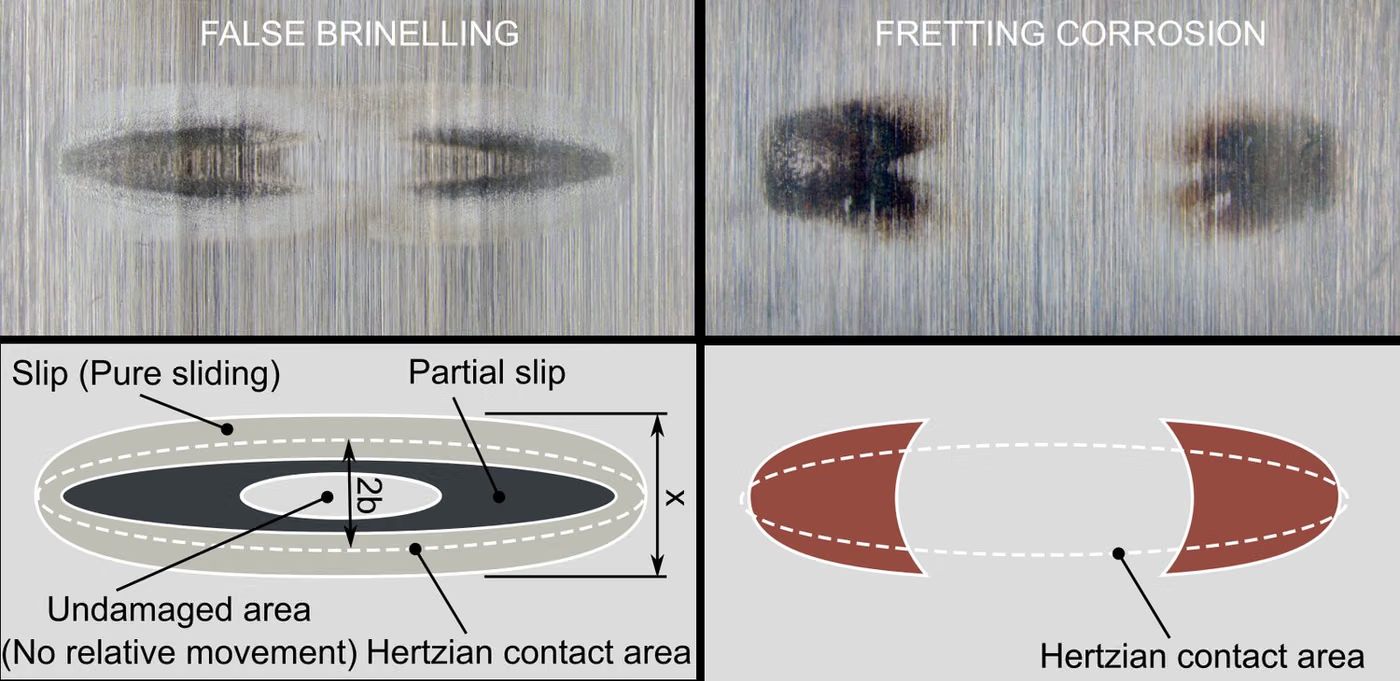
The fretting test is a test in which micron-scale repeated sliding motion is applied between two surfaces pressed together, examining the resulting surface damage and wear. It represents the fretting wear and fretting corrosion seen in joints under vibration.
Purpose of Fretting
The purpose is to assess the risk of damage that micro-motion causes on vibration-exposed press-fit and joint surfaces, supporting the choice of material, coating and lubricant.
Which Products Is Fretting Applied To?
- Electrical contacts and connectors
- Bearing and journal surfaces
- Press-fit joints
- Automotive vibration-exposed fasteners
- Grease and lubricant formulations
In Which Sectors Is Fretting Used?
Standards Related to Fretting
- ASTM G204
- ASTM D4170
- ISO 22696
Fretting Conditions
- Slip amplitude
- Amplitude on the order of microns, as defined (typically 10–100 µm)
- Frequency
- Frequency of repeated motion defined in the specification
- Normal load
- Constant load representing the contact pressure
- Number of cycles
- Defined in the specification
Equipment for Fretting
- Fretting test machine
- High-resolution displacement and force measurement system
- Optical microscope and profilometer
- Contact-resistance measurement rig (for electrical contacts)
Sample Requirements for Fretting
- The contact pair must represent the real application
- Surface roughness and coating thickness must be recorded
- For electrical contacts, the initial contact-resistance value must be measured
- Generally at least three repetitions
Duration of Fretting
It depends on the number of cycles. Tests with hundreds of thousands of cycles can take several days.
Fretting Procedure
- 1The contact pair is prepared and initial values are measured.
- 2Normal load is applied and the amplitude is set.
- 3Repeated motion is started at the defined frequency.
- 4Friction force, and contact resistance if required, are monitored continuously.
- 5Once the cycles are complete, the surfaces are examined with a microscope.
- 6The wear track, oxide build-up and damage type are evaluated.
Fretting Acceptance Criteria
The acceptance criterion is given in the specification as a maximum increase in contact resistance, a maximum wear depth, or the absence of damage after a specified number of cycles.
Evaluation of Results
Fretting damage generally manifests as oxide-debris accumulation and local surface degradation. In electrical contacts, an increase in contact resistance is the primary indicator.
Fretting Report
- Standard applied
- Amplitude, frequency, load and number of cycles
- Contact pair and coating information
- Friction, and contact-resistance, curves if applicable
- Surface-damage images and track profile
Accreditation
EUROLAB holds internationally recognised accreditation obtained from accreditation bodies party to the IAF and ILAC multilateral recognition arrangements, under ISO/IEC 17025 for laboratory testing, ISO/IEC 17020 for inspection and surveillance, and ISO/IEC 17021-1 and ISO/IEC 17065 for system and product certification. This chain ensures the reports and certificates issued are accepted worldwide.
Whether this test can be offered within accredited scope depends on your product and the standard applied; since accreditation is method-based, the scope is confirmed in writing at the quotation stage.
Scope and authorisationsRelated Regulations
- Connector and fastener specifications
- Automotive OEM standards
Mekanik Testler — What Does This Testing Field Cover?
The section below describes the field that the Fretting test belongs to; the conditions and acceptance criteria of this particular test are given in the sections above. The scope specific to your product is confirmed in writing at the quotation stage.
Mechanical testing measures how a material or a part behaves under force. The family ranges from static loading (tension, compression, bending) to time-dependent behaviour (fatigue, creep), and from hardness and wear to fracture toughness.
What these tests have in common is that the result is reported as a MATERIAL PROPERTY. Yield strength or hardness is not a conformity decision; it is numerical data against which the design and the product standard will compare. Mechanical test reports are therefore usually an input to an engineering decision rather than to a product approval — material selection, safety factor, life prediction.
The distinction between static and dynamic behaviour is the key to understanding the field. A part may appear entirely unstressed under a static load yet break under repeated loading; fatigue fracture occurs at stresses well below the yield strength and gives no warning. For rotating, vibrating or cyclically loaded parts, a tensile test alone is therefore not sufficient evidence.
Test conditions determine the result, and this is critical for the readability of the report: specimen geometry, loading rate, temperature, conditioning and the gripping arrangement. The same material gives different values under different conditions. In plastics the rate effect is very pronounced, in metals the temperature effect; in composites the specimen orientation changes the result entirely.
Hardness is the most misused measurement in the field. Because it is fast, close to non-destructive and inexpensive, it is often used in place of strength. Conversion tables from hardness to strength exist, but they are APPROXIMATE and depend on the material group; using them as the sole evidence in material acceptance is wrong.
The fracture mechanics side requires a specific competence. Fracture toughness and fatigue crack growth rate measurements make it possible to calculate how long a cracked structure will last; they are the basis of damage-tolerant design in fields such as pressure equipment, aircraft structures and pipelines.
Method groups in this field
Static tests
Tension, compression, bending, shear and torsion. Yield and tensile strength, elongation and modulus of elasticity are obtained.
Impact tests
Charpy and Izod notch impact; the brittle-to-ductile transition behaviour of the material is determined as a function of temperature.
Hardness
Brinell, Vickers, Rockwell, Shore and micro hardness. Valuable for surface treatment depth and local differences in strength.
Fatigue
Force- and strain-controlled axial fatigue, fatigue in bending; S-N curves and the endurance limit.
Creep and stress relaxation
Behaviour under long-term load at high temperature; decisive for boiler, turbine and pressure equipment materials.
Fracture mechanics
Plane-strain fracture toughness, the J integral, CTOD and fatigue crack growth rate.
Wear and friction
Taber and rotating drum abrasion, coefficient of friction measurements.
Commonly confused in this field
- Calculating strength from hardness is approximate; it cannot be used as the sole evidence in material acceptance.
- Adequate static strength does not demonstrate fatigue strength; a cyclically loaded part requires a separate test.
- If test rate and temperature are not reported, the result cannot be compared — especially for polymers and composites.
- A test specimen and the actual part may not give the same value; moulding orientation, weld lines and differences in surface treatment all have an effect.
- A strength value given for a composite without stating the specimen orientation is meaningless.
- ASTM and ISO counterparts measure the same quantity but use different specimen geometries; the results are not treated as directly equivalent.
Which decisions these results support
- Design verification and material selection
- Incoming material control and supplier approval
- Meeting the mechanical requirements of the product standard
- Failure analysis, life prediction and damage tolerance calculation
- Verifying heat treatment and surface treatment processes
Related Tests
Frequently Asked Questions About Fretting
What is the difference between fretting and normal wear?
Fretting occurs when the slip amplitude is much smaller than the contact area. Wear debris cannot escape the contact zone and accumulates; the damage mechanism therefore differs from continuous sliding.