
What Is Random Vibration — IEC 60068-2-64?
The random vibration test is one in which broadband random vibration in a defined power spectral density (PSD) profile is applied to the sample. It represents vehicle, aircraft and machinery environments more realistically than sine vibration.
Purpose of Random Vibration — IEC 60068-2-64
The purpose is to verify fatigue strength by applying, in accelerated form, the vibration that will be encountered over the service life.
Which Products Is Random Vibration — IEC 60068-2-64 Applied To?
- Automotive electronics
- Aerospace avionics
- Battery modules
- Rail equipment
- Packaged shipment
In Which Sectors Is Random Vibration — IEC 60068-2-64 Used?
Standards Related to Random Vibration — IEC 60068-2-64
- IEC 60068-2-64random vibration test test
Random Vibration — IEC 60068-2-64 Conditions
- PSD profili
- Defined in the specification; Frequency-amplitude curve in g²/Hz
- Toplam rms ivme
- Grms value calculated from the profile
- Time
- Duration per axis as defined (on the order of hours)
- Axis
- Separately in three orthogonal axes
Equipment for Random Vibration — IEC 60068-2-64
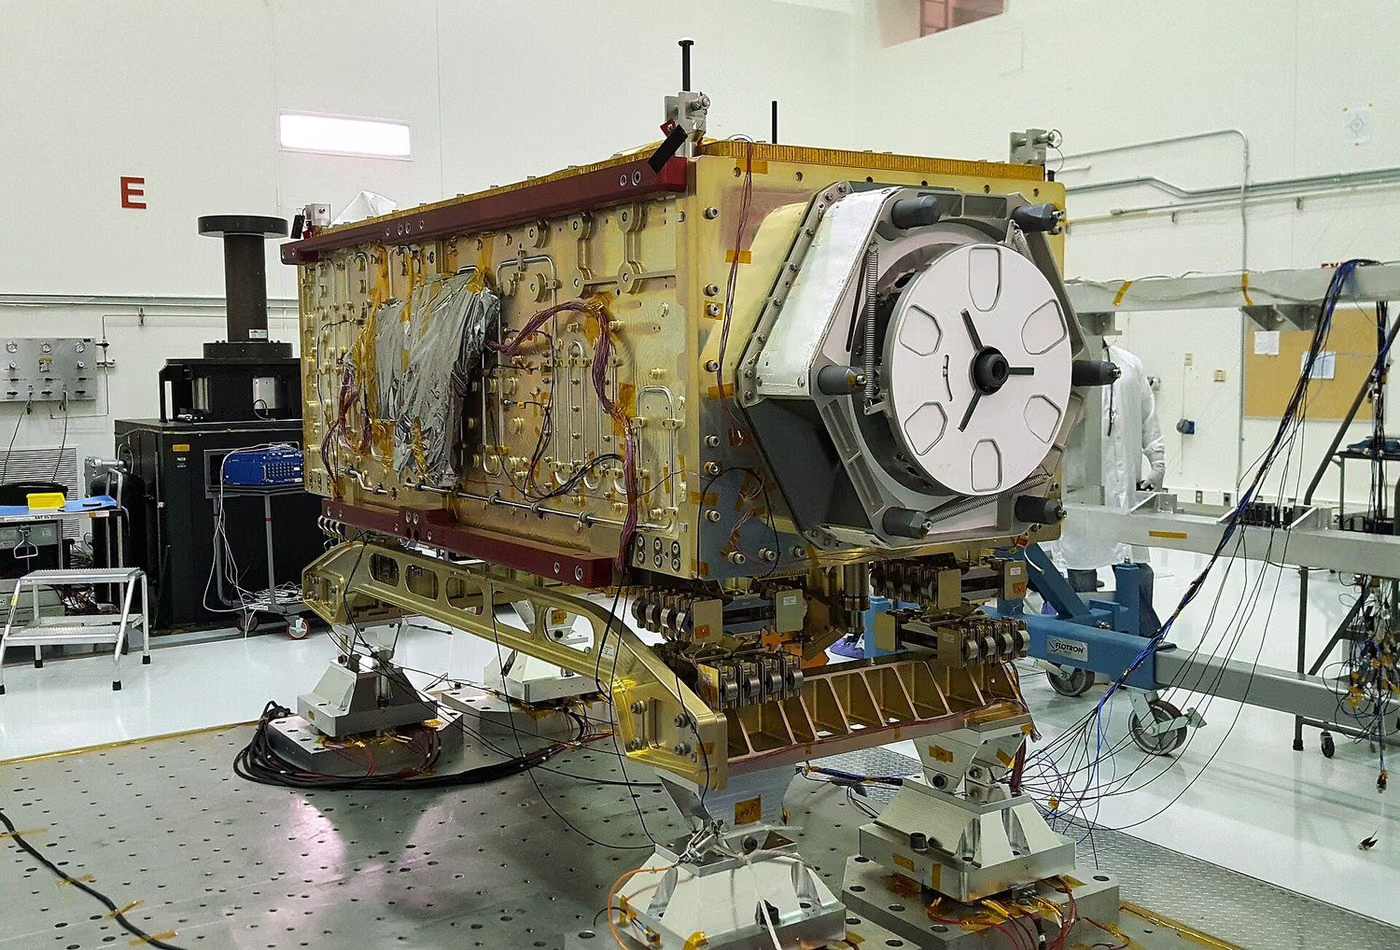
- Electrodynamic shaker and power amplifier
- Multi-channel vibration control system
- Mounting fixture
- Function monitoring
Sample Requirements for Random Vibration — IEC 60068-2-64
- Fixture resonance must lie outside the test band
- The control strategy (single/multi-point) must be defined
- Resonance search must be performed before and after the test
- Function monitoring must be set up
Duration of Random Vibration — IEC 60068-2-64
Typically several days due to the per-axis duration and three axes.
Random Vibration — IEC 60068-2-64 Procedure
- 1The specimen is mounted on the fixture and accelerometers are placed.
- 2A pre-test resonance search is performed.
- 3The PSD profile is loaded and verified within tolerance.
- 4The defined duration is applied on each axis.
- 5The frequency shift is assessed with a final resonance search.
- 6Function and visual inspection are carried out.
Random Vibration — IEC 60068-2-64 Acceptance Criteria
The acceptance criterion is defined in the specification: no structural damage, continuity of function, and no shift in resonance frequency beyond the specified limit.
Evaluation of Results
The measured PSD must remain within the profile tolerance. Frequency shift indicates cracking or loosening.
Random Vibration — IEC 60068-2-64 Report
- Applied standard and PSD profile
- Grms and duration
- Axis information and fixture description
- Pre-/post-test resonance search results
- Functional status
Accreditation
EUROLAB holds internationally recognised accreditation obtained from accreditation bodies party to the IAF and ILAC multilateral recognition arrangements, under ISO/IEC 17025 for laboratory testing, ISO/IEC 17020 for inspection and surveillance, and ISO/IEC 17021-1 and ISO/IEC 17065 for system and product certification. This chain ensures the reports and certificates issued are accepted worldwide.
Whether this test can be offered within accredited scope depends on your product and the standard applied; since accreditation is method-based, the scope is confirmed in writing at the quotation stage.
Scope and authorisationsRelated Regulations
- UNECE R10 and automotive OEM specifications
- Aerospace and rail equipment requirements
Vibration and Shock — What Does This Testing Field Cover?
The section below describes the field that the Random Vibration test belongs to; the conditions and acceptance criteria of this particular test are given in the sections above. The scope specific to your product is confirmed in writing at the quotation stage.
Vibration and shock testing shows whether a product withstands mechanical dynamic loads. The two phenomena are distinct: vibration is a continuous and repeated loading, while shock is a single instantaneous impact at high acceleration. They produce different failure modes and are required separately.
The failure produced by vibration is FATIGUE: a solder joint cracks, a cable sheath abrades, a screw loosens, a connector loses contact. The failure produced by shock is FRACTURE: a brittle component shatters, a bracket breaks, a board comes out of its holder. Testing a product under vibration therefore does not show that it also withstands shock.
Vibration is applied in three forms, each giving different information. Sine vibration sweeps at a single frequency; it is used to find the resonant frequencies of the product and is very valuable at the design stage. Random vibration represents the broadband nature of the real environment and is preferred as evidence of durability. Sine-on-random and random-on-random profiles simulate together the broadband noise superimposed on dominant frequencies from engines and rotors — this is necessary in helicopter and turboprop applications.
RESONANCE is the concept at the centre of the field. Every structure has its own natural frequencies; as the excitation frequency approaches one of them the amplitude grows and the product is exposed to an acceleration many times the input level. A resonance search is therefore carried out before the test, and a design change often takes the form of shifting the resonance rather than lowering the level.
In this family the FIXTURE is part of the result, and this is the most frequently overlooked point. How the specimen is attached to the shaker directly changes the energy transmitted and the resonance behaviour. A poorly designed fixture brings its own resonances into play and imposes a load the product would not otherwise see, or conversely damps the real load and protects the product. Results obtained with different fixtures cannot be compared.
The choice of measurement point also determines the result. The control accelerometer is placed on the fixture and monitoring accelerometers at critical points of the product; the report must document these positions. Accelerations measured at different points in the same test can differ markedly.
Profiles are divided by application area: transport vibration (packaging and shipping), vehicle vibration (by mounting location), rail (EN 61373 categories), aviation (DO-160 sections), military (MIL-STD-810 methods) and battery transport (UN 38.3 T3). The same product passes through different profiles under different programmes.
Method groups in this field
Sine vibration
Determining resonances by frequency sweep and withstand at defined frequencies; the most informative test at the design stage.
Random vibration
Durability with a broadband power spectral density profile; the approach that best represents the real environment.
Combined profiles
Sine-on-random and random-on-random; for dominant frequencies arising from rotating machinery.
Classical shock
Defined acceleration and duration with half-sine, sawtooth and trapezoidal pulse shapes.
Free fall and toppling
Realistic drop scenarios arising from handling; decisive for portable products.
Resonance search and monitoring
Detection of structural change (cracking, loosening) by sweeps before and after the test.
Commonly confused in this field
- Shock and vibration are not the same test; one produces fracture and the other fatigue, and they are required separately.
- A report that does not document the fixture cannot be compared; a fixture can bring its own resonance into play.
- Levels come from the product standard or the programme specification; the standard does not define a single universal level.
- Without a resonance sweep before and after the test, structural damage can go unnoticed; the product may appear to work while being cracked internally.
- The position of the measurement point must be reported; accelerations measured at different points in the same test differ markedly.
- If the product is not operated during the test, intermittent loss of contact remains invisible.
Which decisions these results support
- Verification of transport and in-use durability
- Transport and vehicle vibration conformity for batteries
- Rail, aviation and defence qualification files
- Root cause analysis of solder, connector and joint failures
- The decision to shift a resonance through a design change
Related Tests
Frequently Asked Questions About Random Vibration — IEC 60068-2-64
According to which standard is Random Vibration made?
Random Vibration is executed in scope IEC 60068-2-64, MIL-STD-810 Method 514, RTCA DO-160 Section 8, ISO 16750-3 and IEC 61373. The limit values and acceptance criteria to be applied are defined in the product standard; The version valid for your product is confirmed in writing at the offer stage.
Which products does Random Vibration apply to?
Mainly applied to Automotive electronics, Aerospace avionics, Battery modules, Rail equipment and Packaged shipment. Whether your product is included in the scope is determined by examining its technical specifications and intended use.
Under what conditions is Random Vibration done?
The determining parameters are: PSD profili — Defined in the specification; Frequency-amplitude curve in g²/Hz, Toplam rms ivme — Grms value calculated from the profile and Time — Duration per axis as defined (on the order of hours). The full terms are in the "Test Conditions" section on the page and vary depending on the product standard.
What kind of sample is needed for Random Vibration?
Fixture resonance must lie outside the test band, The control strategy (single/multi-point) must be defined and Resonance search must be performed before and after the test. The number of samples is determined according to the product standard and the scope to be reported.
How long does Random Vibration take?
Typically several days due to the per-axis duration and three axes. This duration belongs to the experiment itself; sample preparation, queuing and reporting are also evaluated. A realistic schedule for your product is given in the offer.
What is the Random Vibration result called "appropriate"?
The acceptance criterion is defined in the specification: no structural damage, continuity of function, and no shift in resonance frequency beyond the specified limit.