
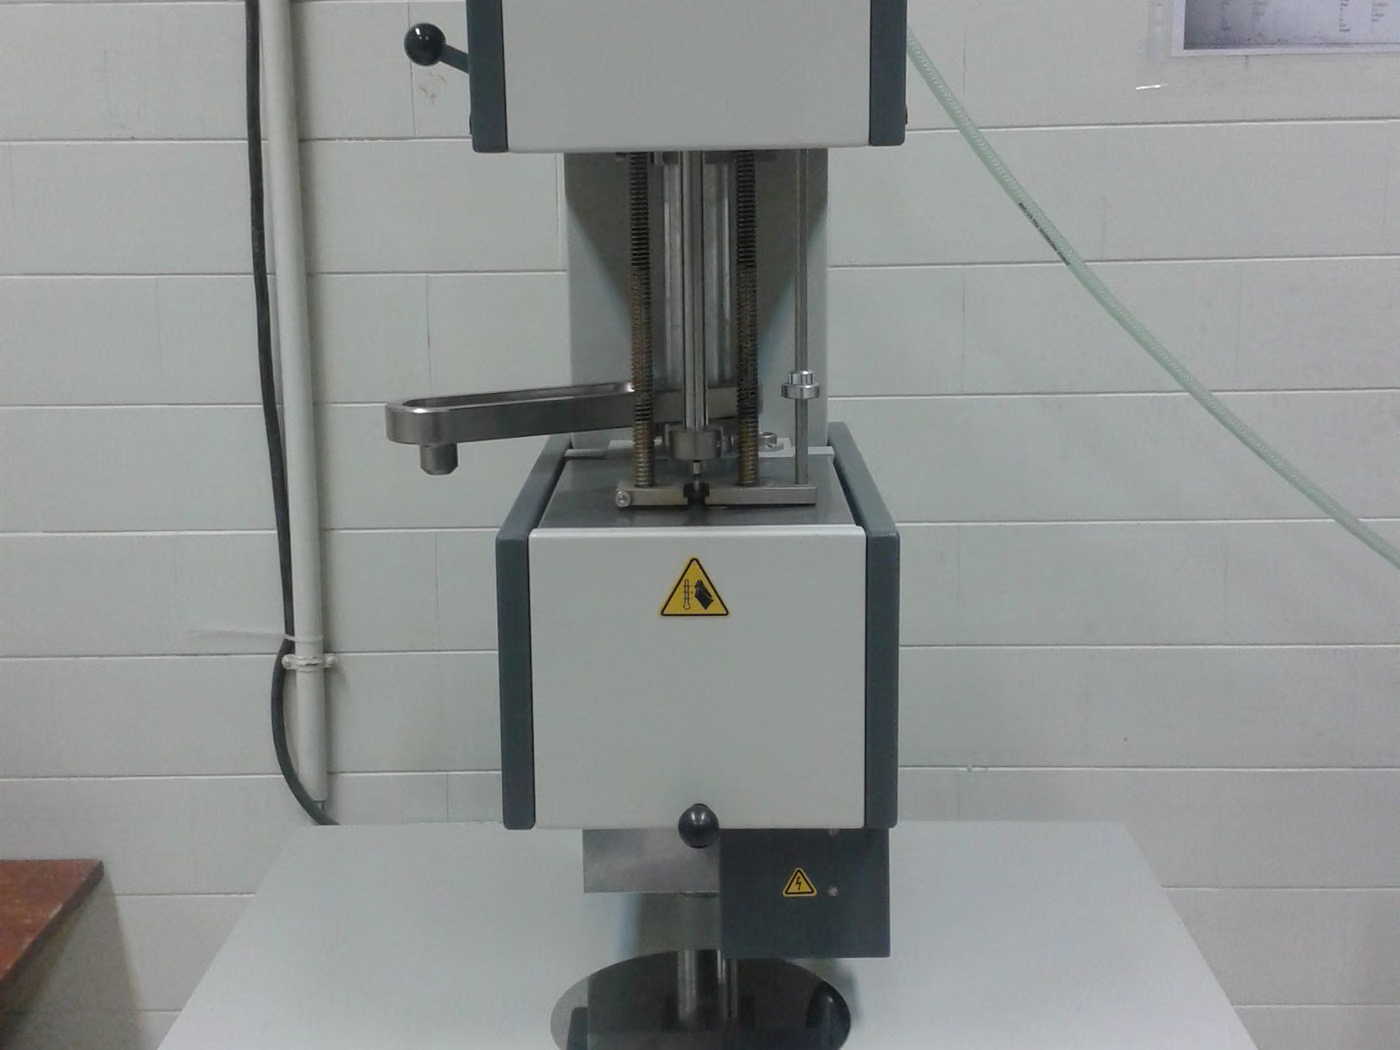
What Is MFI/MFR?
Melt flow index test is an experiment in which the mass (MFR, g/10 min) or volume (MVR) of the thermoplastic material flowing through a standard capillary mold in ten minutes under defined temperature and piston load is measured.
Purpose of MFI/MFR
The aim is to verify batch consistency and suitability for processing by monitoring the polymer's flow behavior and indirectly its molecular weight.
Which Products Is MFI/MFR Applied To?
- Polyethylene and polypropylene raw materials
- Injection and extrusion granules
- recycled polymers
- Masterbatch and additive mixtures
In Which Sectors Is MFI/MFR Used?
Standards Related to MFI/MFR
- ISO 1133-1
- ISO 1133-2
- ASTM D1238
MFI/MFR Conditions
- Temperature
- Defined in the standard according to polymer (e.g. 190 °C for PE, 230 °C for PP)
- Load
- Piston load defined in the standard (e.g. 2.16 kg or 5 kg)
- Pattern
- Standard capillary die dimensions
- Kurutma
- Hygroscopic polymers must be dried before measurement
Equipment for MFI/MFR
- Melt flow index device (plastometer)
- Caliber weight set
- Analytical balance
- drying oven
Sample Requirements for MFI/MFR
- The sample must be in granular or ground form
- Hygroscopic polymers must be dried under the condition defined in the standard.
- Temperature and load should be selected according to material standard
- A sufficient number of cuts must be taken
Duration of MFI/MFR
Typically 1–2 days, including specimen preparation.
MFI/MFR Procedure
- 1Numune gerekiyorsa kurutulur.
- 2The device is brought to the target temperature and equilibrated.
- 3The sample is filled into the cylinder and preheated.
- 4Piston load is applied.
- 5At defined intervals, cuttings are taken and weighed.
- 6MFR or MVR is calculated.
MFI/MFR Acceptance Criteria
The acceptance criterion is the MFR range given in the material standard or specification.
Evaluation of Results
If the temperature and load combination changes, the result is not comparable; The report must contain these two parameters. Moist sample measurement gives falsely high MFR due to hydrolytic degradation.
MFI/MFR Report
- Standard applied
- Temperature and load
- Drying conditions
- Cutting masses and MFR/MVR value
- Assessment against the material standard
Accreditation
EUROLAB holds internationally recognised accreditation obtained from accreditation bodies party to the IAF and ILAC multilateral recognition arrangements, under ISO/IEC 17025 for laboratory testing, ISO/IEC 17020 for inspection and surveillance, and ISO/IEC 17021-1 and ISO/IEC 17065 for system and product certification. This chain ensures the reports and certificates issued are accepted worldwide.
Whether this test can be offered within accredited scope depends on your product and the standard applied; since accreditation is method-based, the scope is confirmed in writing at the quotation stage.
Scope and authorisationsRelated Regulations
- Material product standards and procurement specifications
Plastics Testing — What Does This Testing Field Cover?
The section below describes the field that the MFI/MFR test belongs to; the conditions and acceptance criteria of this particular test are given in the sections above. The scope specific to your product is confirmed in writing at the quotation stage.
Plastics testing determines the mechanical, thermal and burning behaviour of a polymer material. Unlike metals, plastics are VISCOELASTIC: their behaviour depends on loading rate, temperature and moisture. The same material therefore gives different results under different conditions, and the test conditions are an inseparable part of the result.
The practical consequence of viscoelasticity is this: a plastic part continues to deform over time under a constant load (creep) and the stress it carries at constant deformation falls over time (stress relaxation). A screwed joint loosens, a clamp loses its clamping force, a shelf sags over time. A short-term tensile test does not show this behaviour; a long-term test or an accelerated model is needed.
Thermal behaviour is the second main axis. Melt flow rate indicates the processability of the material and lot-to-lot consistency; heat deflection temperature and the Vicat softening point give a rough limit for service temperature. Thermal analysis (DSC, TGA, DMA) reveals the identity of the material: glass transition temperature, melting behaviour, crystallinity, filler content and decomposition temperature.
Burning behaviour is the third axis and ties directly into product standards. The UL 94 class and the limiting oxygen index are written into the material data sheet; a particular class is required for the housing of an electrical appliance, while a different classification system applies to a construction product.
Ageing is the most frequently skipped part of the field. Plastics degrade under UV, heat, moisture and oxygen: colour changes, the surface cracks, impact strength falls. For a part intended for outdoor use, what matters is not its values on day one but its values after ageing. Xenon arc and fluorescent UV equipment accelerate this degradation and allow comparison.
The output of this family is usually written into the material data sheet, and product standards refer to that sheet. But there can be a difference between the data sheet value and the behaviour of the actual part: orientation formed during moulding, weld lines and internal stresses make the part behave differently from the specimen.
The use of recycled content has added a new question to the field. Recycled resin varies from lot to lot; mechanical properties, colour and burning behaviour can shift between batches. For a manufacturer using recycled material, incoming material control is therefore not a choice but a necessity.
Method groups in this field
Mechanical
Tension, compression, bending, Charpy and Izod impact, hardness (Shore), creep and environmental stress cracking.
Thermal
Melt flow index (MFI), heat deflection temperature (HDT), Vicat softening temperature, linear thermal expansion.
Thermal analysis
Transition temperatures and crystallinity by DSC, composition and decomposition by TGA, dynamic mechanical behaviour by DMA.
Burning
UL 94 classification, limiting oxygen index (LOI), glow wire and needle flame tests.
Ageing
Accelerated ageing by xenon arc and fluorescent UV, hot air ageing, humidity and condensation.
Physical
Density, water absorption, ash content, gas and water vapour permeability of films and sheets.
Commonly confused in this field
- A plastics result without a stated test rate and temperature cannot be interpreted; viscoelastic behaviour depends on these parameters.
- A specimen result does not transfer directly to the actual part; moulding orientation and weld lines are decisive.
- HDT and Vicat values are NOT service temperatures; they are a rough indication of an upper limit and do not apply under load.
- The UL 94 class depends on thickness; a different wall thickness requires re-verification.
- For moisture-absorbing polymers (such as polyamide), results are misleading unless conditioning is carried out.
- ASTM D638 and ISO 527 results are not directly equivalent; the specimen geometries and rate definitions differ.
Which decisions these results support
- Material selection and supplier approval
- Meeting the flammability and thermal requirements of the product standard
- Verifying the use of recycled content and lot control
- Moulding process control and lot consistency
- Demonstrating ageing resistance for outdoor use
Related Tests
Frequently Asked Questions About MFI/MFR
Does the MFR value give the molecular weight?
It does not give directly but is inversely related: higher MFR generally indicates lower molecular weight. Quantitative molecular weight requires gel permeation chromatography.